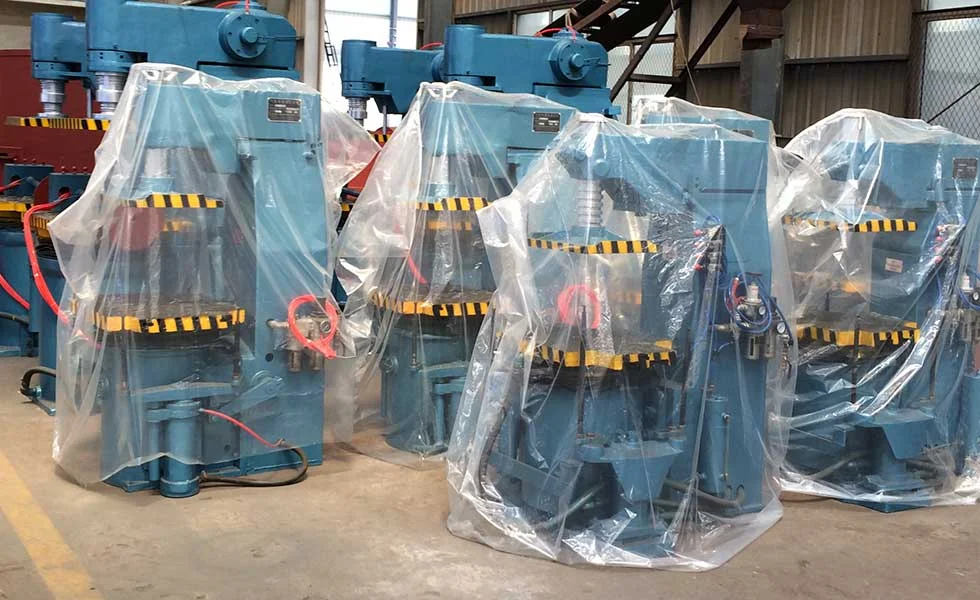
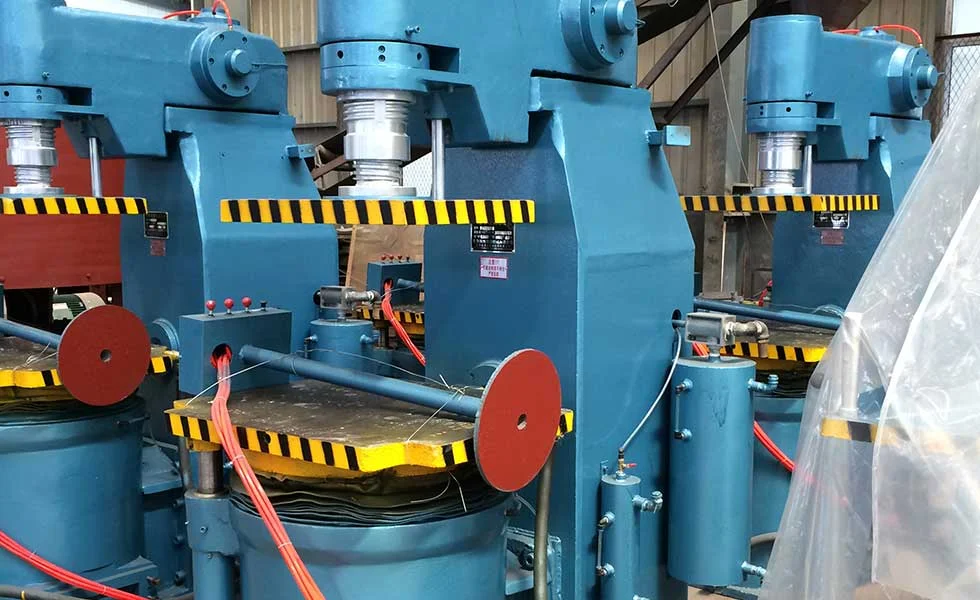
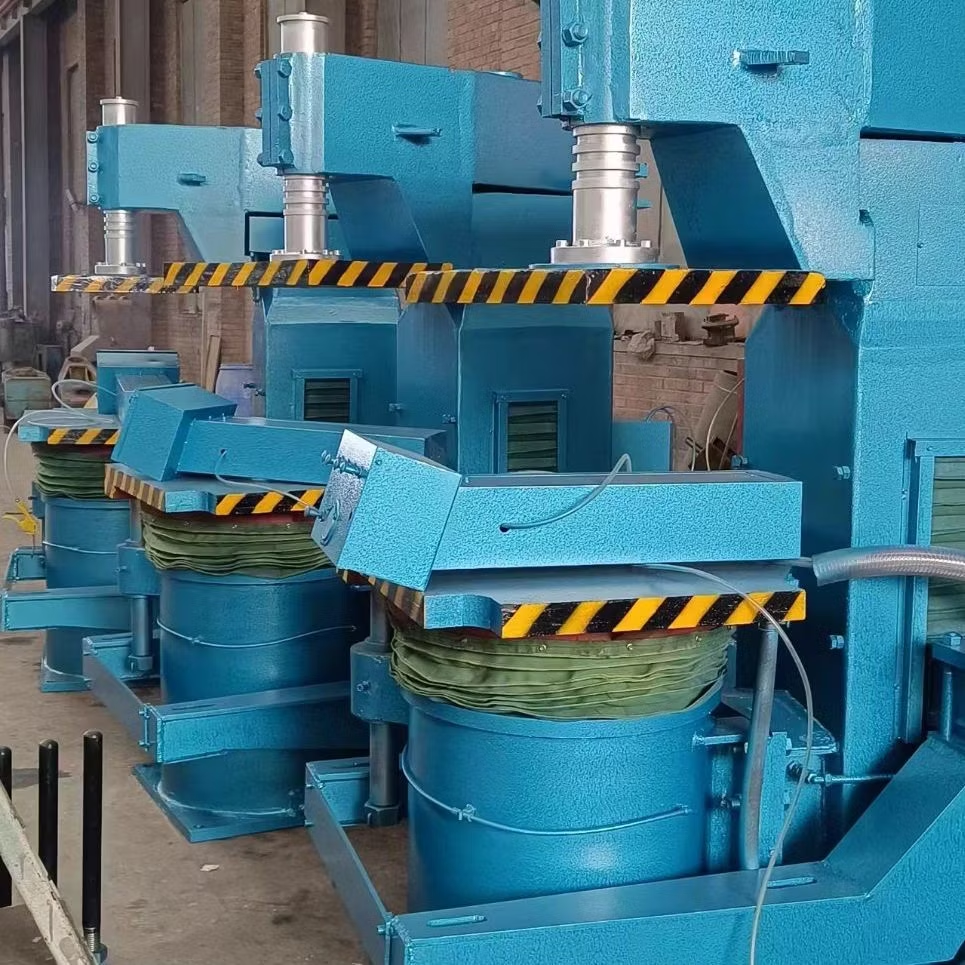
Jolt Squeeze Molding Machine
Uneven compaction causes casting defects. We help you mold faster and firmer — from a factory that understands foundry work.
Built to solve loose sand and weak molds, our jolt squeeze machine delivers strong, consistent compaction — improving surface quality and cutting down rework.
About Jolt Squeeze Molding Machine Overview
The factory-built Jolt Squeeze Molding Machine combines jolting and squeezing to compact green sand for foundry molding. Compaction quality depends on flask and pattern geometry, sand properties, machine settings and the selected cycle.
Select the model using the required squeeze force and stroke, the actual flask envelope and the loading arrangement. Mold quality and productivity are evaluated under the agreed process and acceptance conditions; uniform compaction of every possible geometry is not assumed.
We offer a range of significant benefits:
Jolting and squeezing support green-sand compaction. Mold acceptance depends on sand condition, flask/pattern geometry and the selected operating cycle.
Complex patterns require review of the actual flask envelope, press-head clearance, draw stroke and sand-compaction requirements.
Manual ramming requires high experience and is prone to variation. This system standardizes the compaction process, ensuring consistency even with less-experienced operators.
Every minute counts. Compared to manual or low-pressure methods, our machine shortens cycle times and improves throughput — especially in small to mid-volume casting jobs.
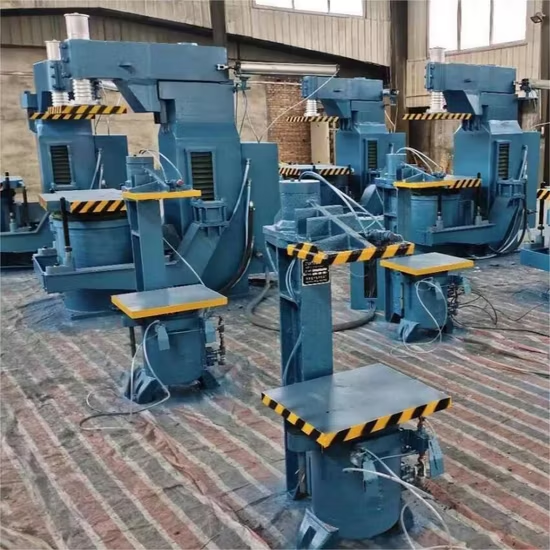
As the equipment manufacturer, we design for real foundry conditions. Rugged structure, easy maintenance access, and model flexibility let you integrate fast and run steady from day one.
Get a Quote
Comprehensive Support and ServicesAlways Providing the Help You Need
When your molding machine isn’t performing as expected, the entire production line suffers — cycle times increase, mold strength becomes inconsistent, and casting defects pile up. Worse yet, without clear guidance or timely technical response, problems linger, operators get frustrated, and productivity takes a hit.
We understand the critical role jolt squeeze molding machines play in your core molding process. That’s why we offer more than equipment — we deliver complete operational support. From on-site installation and parameter setup to operator training and troubleshooting, we help you launch faster, work smarter, and run more reliably.
Our support is not an afterthought — it’s the foundation for keeping your molding machine efficient, consistent, and production-ready every shift.
Technical Specification of Jolt Squeeze Molding Machine - Technical Specifications
Jolt Squeeze Molding — Model and Cycle Definitions
The machine combines jolting and squeezing for green-sand mold compaction. Selection depends on the actual flask, pattern, sand condition, loading method and agreed mold acceptance requirements.
Force and Stroke
| Model | Squeeze force (kgf) | Squeeze stroke (mm) |
|---|---|---|
| Z143W | 4000 | 100 |
| Z144W | 4200 | 120 |
| Z145W | 6300 | 160 |
| Z146W | 7000 | 160 |
| Z147 | 10000 | 250 |
| Z148 | 16000 | 350 |
| Z149 | 18000 | 350 |
| Z1410 | 19000 | 350 |
| Model | Molding / draw stroke (mm) | Reference worktable (mm) |
|---|---|---|
| Z143W | 160 | 560×420 |
| Z144W | 150 | 560×465 |
| Z145W | 200 | 610×515 |
| Z146W | 200 | 700×550 |
| Z147 | 250 | 880×700 |
| Z148 | 350 | 1000×800 |
| Z149 | 350 | 1100×900 |
| Z1410 | 350 | 1400×1030 |
Terminology: kgf is a force unit, not stress. Molding / draw / pattern-stripping stroke is not the true jolt vibration amplitude. Actual vibration amplitude requires drawing confirmation.
Workpiece acceptance: Worktable size is a reference dimension, not maximum allowable flask size. Confirm the ordered variant, press-head clearance and draw stroke in the selected GA before accepting a flask or pattern. Z145W has alternative worktable dimensions; the Z147 reference is approximate.
Air Consumption and Reference Productivity
| Model | Air (m³/box) | Reference rate (boxes/h) |
|---|---|---|
| Z143W | 0.25 | 40–60 |
| Z144W | 0.35 | 40–60 |
| Z145W | 0.40 | 40–60 |
| Z146W | 0.40 | 40–60 |
| Z147 | 0.60 | 40–60 |
| Z148 | 0.60 | 40–60 |
| Z149 | 0.60 | 25–40 |
| Z1410 | 0.60 | 25–40 |
One box: One upper OR one lower molding-box machine cycle. A cope-and-drag pair requires two box cycles; these figures are not complete mold-pairs per hour.
Operating conditions: Air consumption must be assessed at the specified supply pressure and stated reference air condition, to be confirmed in the pneumatic documentation. Do not assume a free-air or compressed-volume basis. Reference hourly rates depend on the actual loading, compaction, drawing and unloading cycle and are not guaranteed line output.
Unconfirmed variants and utilities: Z145WB and Z146WB specifications require their own approved model documentation; values are not inferred from W models. Auxiliary electrical power, maximum flask envelope and utility requirements follow the selected equipment BOM and drawings.

Why Choose Us
Unmatched Quality and Innovation
Description: "Tailored solutions designed to meet specific industrial needs
Durable machines built to last, even in the toughest environments
Reduce operating costs with energy-efficient designs
Remote technical support, overseas installation and commissioning, operator training, spare-parts support and emergency technical assistance are available according to project requirements.
Installation guidance, commissioning, training and remote support are available according to project requirements; overseas engineer support is arranged within the agreed scope.
Dust-control arrangements and environmental acceptance requirements depend on the selected configuration and project location.
Enjoy low maintenance costs due to high-quality components
Safety functions and operating requirements are defined for the selected equipment configuration; confirm them in the approved documentation.
What you need
Comprehensive Shot Blasting Systems
Hitech machines are designed and engineered according to our customers’ specific requirements and specifications. Each component is assembled with meticulous attention to quality by our in-house fabrication team, ensuring every unit meets the highest standards

External pipe shot blasting and internal pipe blasting are separate modules that may be integrated into a project line.

Designed for cleaning anchor chains within the selected model and process range; removes rust and scale to prepare the surface.

A dual-station coil-batch system for wire-rod surface cleaning; one station may blast while the other is loaded or unloaded.

The HTJX family is a fixed roller-conveyor line for external steel-pipe surface cleaning, with handling and installation defined by the project.

For medium to large/heavy components within the selected model envelope; total table load includes workpiece and fixtures.

This machine offers efficient cleaning and preparation for roads and large floor areas, suitable for removing road markings, stains, and enhancing roughness to improve traction
Let’s Discuss Your Foundry Needs
We are ready to hear about your needs. Partner with Hitech to create your success story. Contact us to begin the conversation